Skip to content
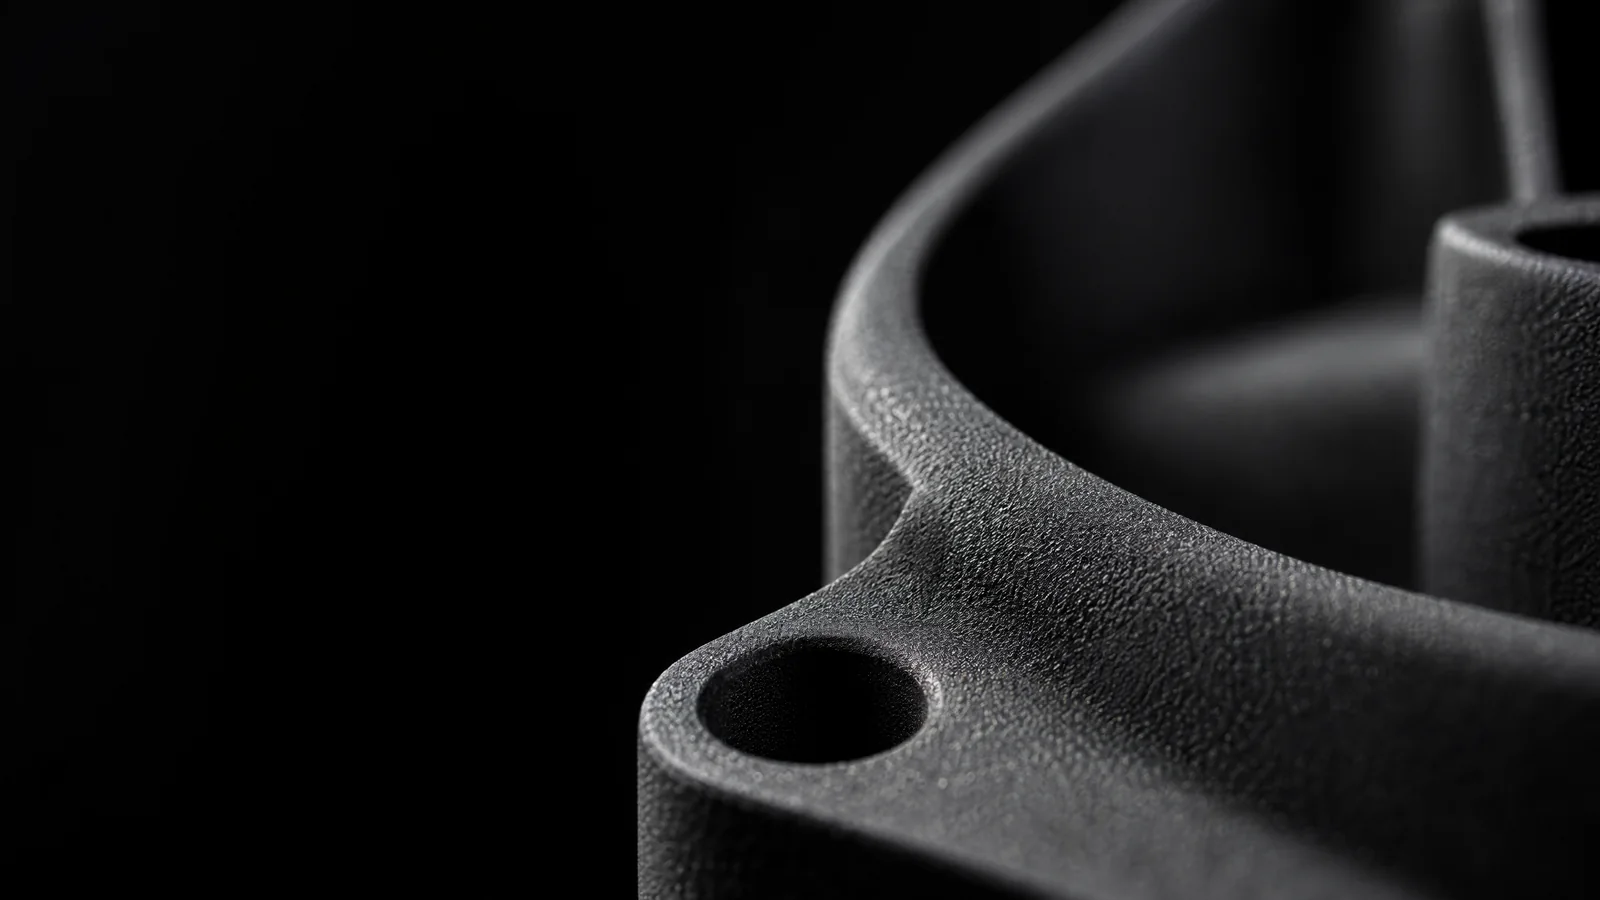
Close-up of a sintered PA12 part: grainy surface, mounting hole and rounded wall

PA12 series parts,
delivered from 24 hours

We manufacture on our own machines in Switzerland, from the first sample to series production, with precise traceability.

Over 1,000 industrial customers,
including

  • Siemens
  • Bosch
  • NVIDIA
  • Logitech
  • Novartis

PA12 series parts from a single source: one plant, one contact, one material.

Same-day productionMade inSwitzerland

  1. 01

    Enquiry

    • By email
    • Via the ordering portal
    • Via API
  2. 02

    Sample part

    • Test the material on your own part
    • Assess the surface finish
  3. 03

    Series production

    • Same powder, same parameters
    • Reorder at any time
  4. 04

    Framework agreementoptional

    • Fixed prices
    • Call-offs as needed

Software for modern manufacturing

One portal for everyone involved with the part: purchasing reorders, engineering releases revisions, quality traces an individual part back. Everyone sees the same, up-to-date status.

Volumetrix PortalSearch part or drawing number
New enquiryRFQ-2026-0412
Quote received
10Holder2045.415.01 · Rev. ASTEP2.4 MBPDF310 kB500 pcs
Material
PA12 black
Requested date
Week 44
Inspection
First article inspection
Quote AN-2026-1187Delivery week 43 · valid until 31/10/2026Open quote

Sample view, simplified. Traceability to follow.

From small batches to high-volume series, made in PA12.

What we are built for

  • Small batches and first orders
  • High-volume series with recurring call-offs
  • Spare parts for product lines in the field
  • Pre-series and pilot runs before launch
One-off parts, other materials and processes
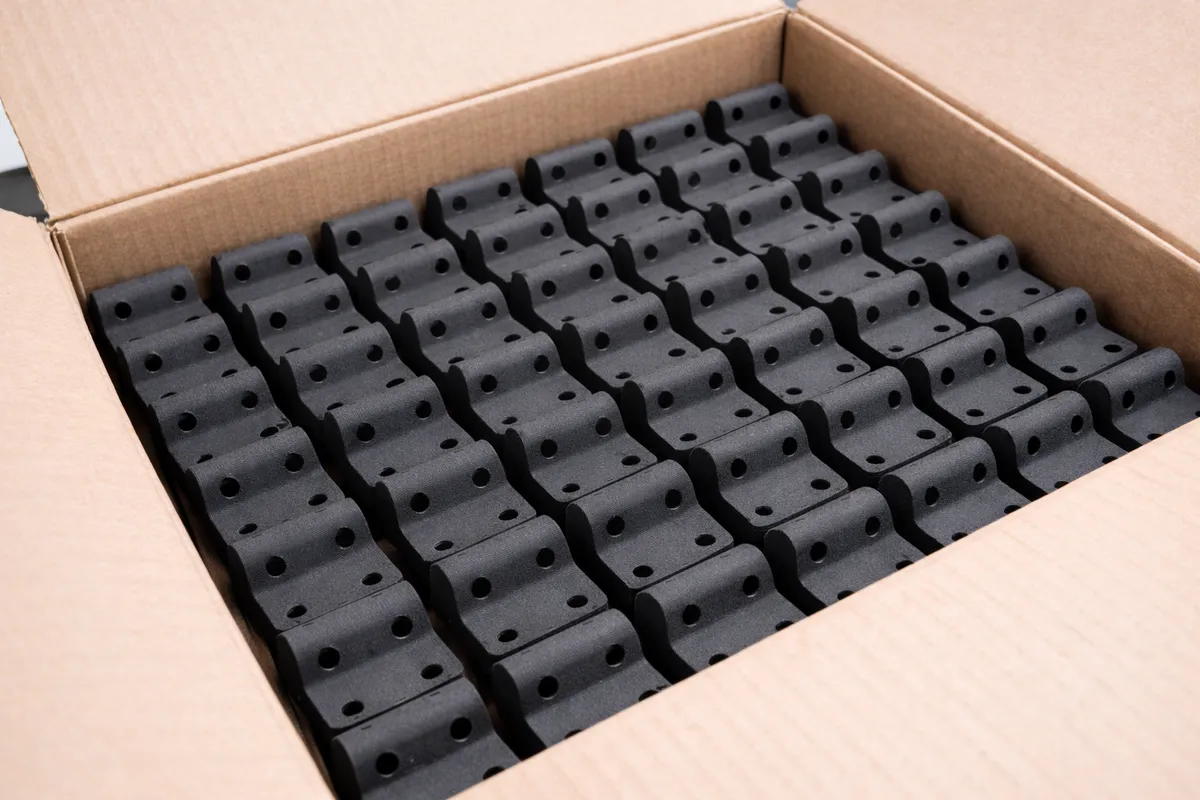
Open carton holding a series of identical black PA12 parts, tightly packed in rows
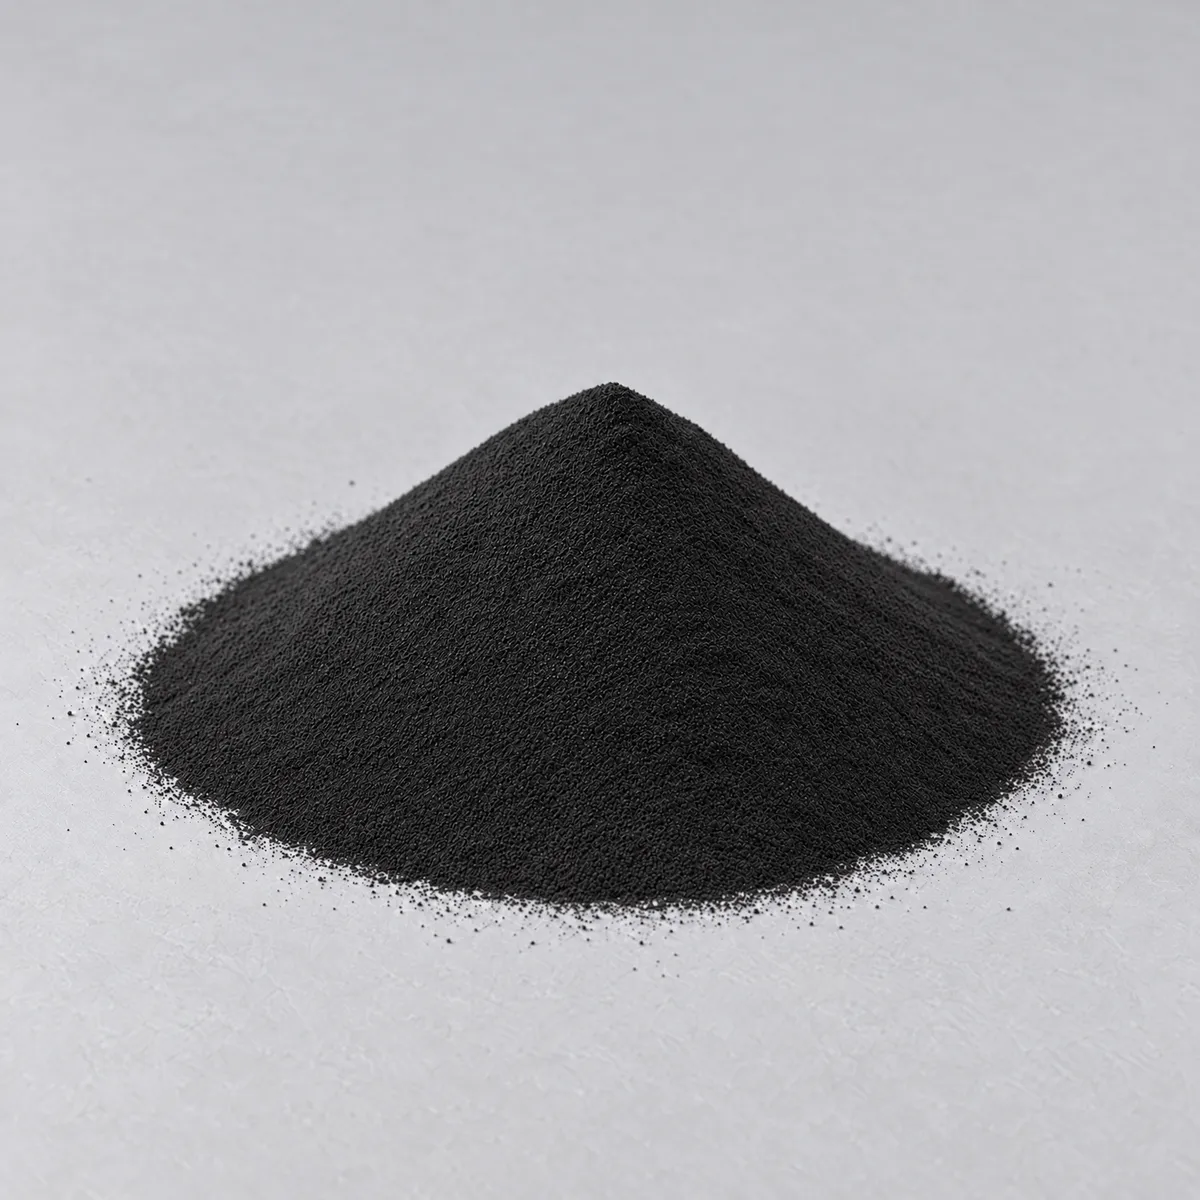
Cone of fine polyamide 12 powder for laser sintering

Polyamide 12

Tough, dimensionally stable and resistant to oils, fuels and most cleaning agents. Sintered without support structures, even with undercuts and internal channels.

Tensile strengthASTM D638
50MPa
Tensile modulusASTM D638
1850MPa
Flexural strengthASTM D790
66MPa
Water absorptionASTM D570
0.66%

Temperature

The temperature up to which the part holds its shape under load

PropertyValue
Heat deflection at 1.8 MPaASTM D64887 °C
Heat deflection at 0.45 MPaASTM D648171 °C
Vicat softeningASTM D1525175 °C

Build orientation

Elongation at break in the build plane and perpendicular to it

PropertyValue
In the build plane, X and YASTM D63811 %
Perpendicular to the build plane, ZASTM D6386 %

Chemical resistance

Weight gain after 24 hours of immersion

PropertyValue
Hydrochloric acid, concentrated0.8 %
Mineral oil, heavy0.7 %
Hydraulic oil0.6 %
Skydrol 50.6 %
Mineral oil, light0.5 %
Diethylene glycol monomethyl ether0.5 %
Diesel fuel0.4 %
Tripropylene glycol monomethyl ether0.3 %
Isopropyl alcohol0.2 %
Sodium hydroxide solution, pH 100.2 %
Hydrogen peroxide 3 %0.2 %
All properties
Mechanical
Tensile strengthASTM D638 Type 150 MPa
Tensile modulusASTM D638 Type 11850 MPa
Elongation at break in X and YASTM D638 Type 111 %
Elongation at break in ZASTM D638 Type 16 %
Flexural strengthASTM D790-1566 MPa
Flexural modulusASTM D790-151600 MPa
Impact strength, notchedASTM D256-1032 J/m
Thermal and other
Heat deflection temperature at 1.8 MPaASTM D64887 °C
Heat deflection temperature at 0.45 MPaASTM D648171 °C
Vicat softening temperatureASTM D1525175 °C
Water absorptionASTM D5700.66 %
FlammabilityUL 94HB
Design guide

Guide values for polyamide 12 on the Formlabs Fuse 1+. Below these, details lose definition, holes can close up and thin webs can break.

  • Wall thickness

    min. 0.6 mm vertical, 0.3 mm horizontal

  • Holes

    Diameter min. 1.0 mm

  • Pins

    Diameter min. 0.8 mm

  • Cavities

    Powder escape holes min. 3.5 mm, two per cavity

  • Moving parts printed in one piece

    Gap 0.3 mm up to 20 mm² area, 0.6 mm above

  • Fit between separate parts

    Clearance 0.2 mm up to 20 mm² area, 0.4 mm above

  • Embossed text

    min. 4.5 mm high, 0.3 mm raised

  • Engraved text

    min. 3.0 mm high, 0.3 mm deep

  • Part size

    up to 160 × 160 × 297 mm

Fine details and spacing
Raised, horizontal surface0.15 mm high, 0.35 mm wide
Raised, vertical surface0.35 mm high, 0.4 mm wide
Recessed, horizontal surface0.1 mm deep, 0.3 mm wide
Recessed, vertical surface0.15 mm deep, 0.35 mm wide
Separate parts in the same buildmin. 1.0 mm apart, 5.0 mm recommended

Manufacturing and post-processing
in-house

We sinter on our own machines and finish every part in our own workshop.

  • DepowderingResidual powder is removed from the part and its cavities.
  • BlastingFor an even, matt surface.
  • Dip dyeingDyed throughout in an immersion bath.
  • PolishingFor a smoother, sealed surface.
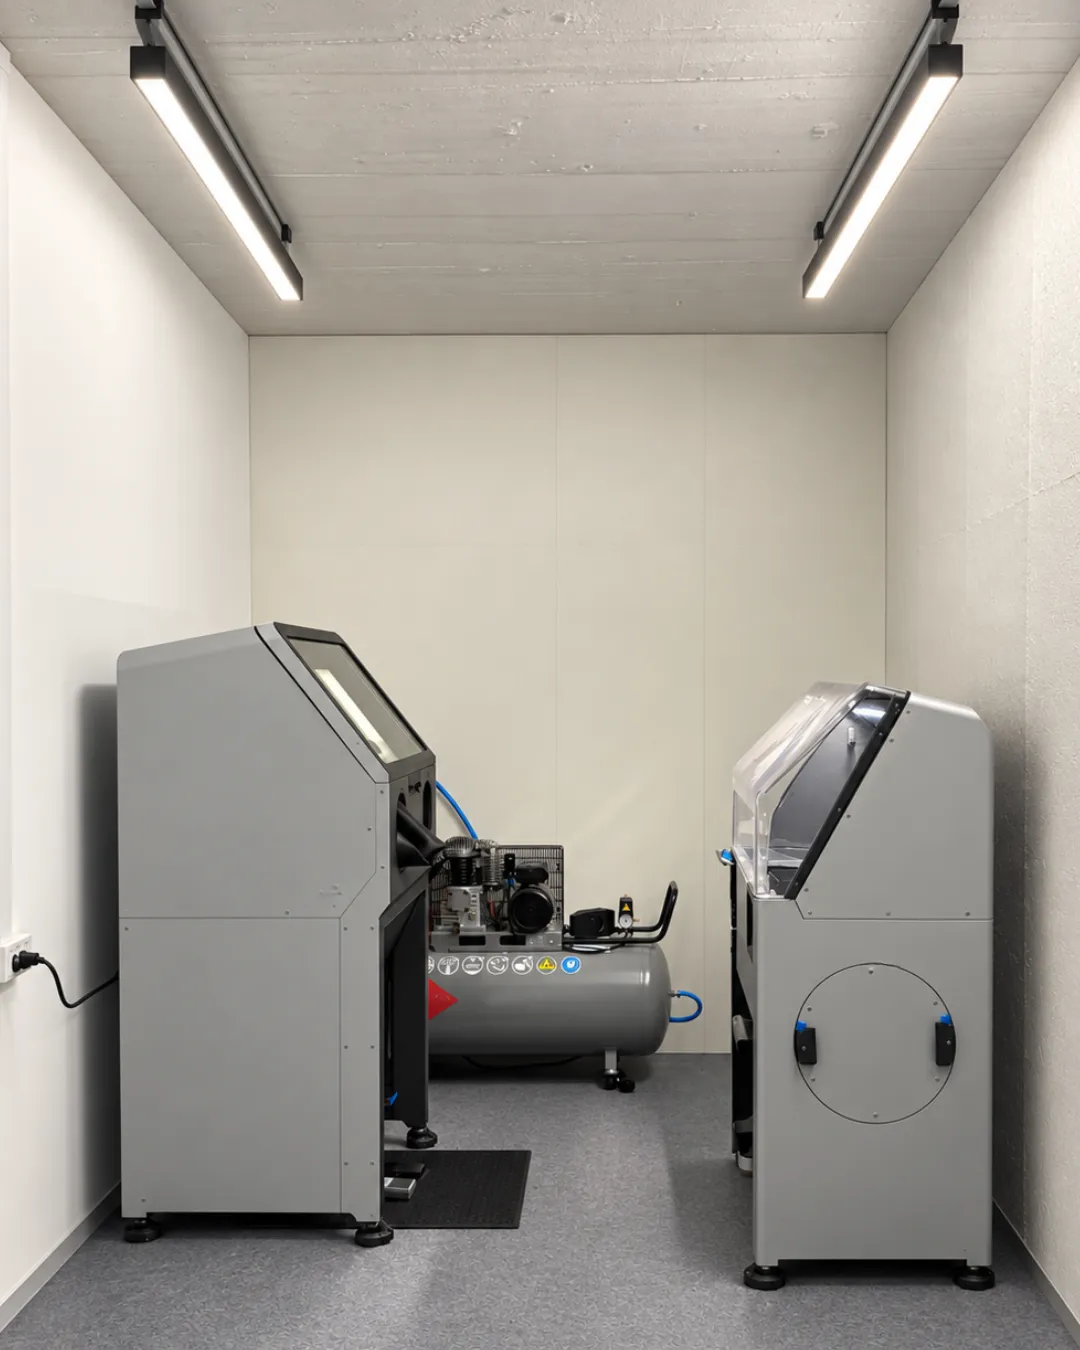
Post-processing workshop with blasting cabinet, compressor and depowdering station

Send an enquiry

Manufacturing, software or something else: tell us briefly what it is about. You will receive a confirmation by email straight away.

Directly by email: info@volumetrix.ch

Type of enquiry
Files
Drag files here or STEP, STL or PDF, up to 10 files, 200 MB each
Fields marked * are required.